BDI: 1,842 ▼ 1.2%
COTTON NO.2: 84.12 ▲ 0.4%
LME COPPER: 8,432.50 ▲ 2.1%
FOOD SAFETY INDEX: 94.2 ARCHIVE_SECURED
OPTICAL INDEX: 11,204.09 STABLE
BDI: 1,842 ▼ 1.2%
SECTOR INDEX
V.24.08 ARCHIVE
Hot Articles
- Tamil Nadu Plans SIM-Based Upgrade for 17.7 Million Smart MetersTamil Nadu plans 17.7 million smart meters with proposed SIM-based upgrades. Explore potential supplier opportunities and the tender details still to come.
- Fiber Laser CE Marking: EU Safety Requirements and DocumentationFiber laser CE compliance goes beyond the mark. Explore EU safety requirements, essential documentation and practical checks before purchasing.
- US Grid Equipment Shortages Could Hinder $1 Trillion UpgradeUS grid equipment shortages could hinder a $1 trillion upgrade. Explore how transformer supply, data centers and rising power demand could affect grid projects.
How Do You Assess Technical Fabric Suppliers?


Assess technical fabric suppliers by linking every performance claim to a defined application, a reproducible test method, and evidence from routine production. A strong laboratory result supports qualification only when the tested material matches the proposed construction, finish, manufacturing site, and delivered condition. Price comparisons become meaningful after these requirements are established.
The assessment should answer three questions: does the fabric perform under the intended conditions, can production maintain that performance, and will each shipment carry enough evidence to verify conformity? This industrial product application guide develops those questions into a practical qualification process covering specifications, test reports, production trials, traceability, and supplier approval.
Define the conditions that determine acceptance
Begin with the fabric’s function and the consequences of failure. Protective clothing, filtration media, and reinforcement fabrics require different evidence, even when their datasheets list similar properties. High tensile strength, for example, does not establish resistance to chemical penetration, particle capture efficiency, or compatibility with a composite resin.
Translate the application into measurable requirements before requesting quotations. Include the operating environment, relevant loads, exposure duration, cleaning or sterilization processes, and downstream conversion. Separate mandatory acceptance limits from preferred characteristics so that an attractive secondary feature cannot compensate for a failure in the primary function.
Define the delivery condition as precisely as the end use. A result obtained on uncoated cloth cannot establish the performance of a coated grade. Likewise, testing a new fabric does not demonstrate performance after repeated laundering. Where service conditions change the material, acceptance testing should include the relevant conditioning sequence.
Read test reports beyond the headline result
Request complete reports for the proposed grade. A summary stating “tested to ISO” or “ASTM compliant” leaves essential questions unanswered: which method, which edition, what specimen, what conditions, and what result? Many test standards describe measurement procedures without setting a universal pass threshold. The acceptance limit must come from the application specification or an applicable product requirement.
Start with sample identity. The report should connect the tested specimen to a fabric designation, composition, construction, finish, and identifiable lot or sample reference. Establish whether it came from development equipment, a specially prepared sample, or normal production. A technically sound report has limited qualification value when its connection to the offered material is unclear.
Next, examine comparability. Tensile results change with specimen geometry, grip arrangement, loading rate, and direction. Air permeability depends on the pressure differential and test area. Abrasion results depend on the apparatus, abrasive medium, loading, and endpoint. Values obtained under different methods should not be placed in a ranking as though they measure identical behavior.
Review conditioning, specimen count, individual results where available, and reported variability. A comfortable average can conceal specimens below the required minimum. If measurement uncertainty is material to a decision near the acceptance boundary, agree on the decision rule before testing.
Independent laboratory testing strengthens confidence when the laboratory’s accredited scope covers the relevant method. Accreditation alone does not establish that every reported test falls within that scope. Supplier laboratory results remain useful for process monitoring, provided the methods, equipment controls, and relationship to qualification testing are documented.
Connect fabric construction to downstream behavior
Composition and fabric weight are insufficient descriptions of a technical textile. Yarn type, filament structure, weave or knit geometry, nonwoven bonding, coating chemistry, and finishing conditions influence performance. Two fabrics with the same nominal fiber content and mass per unit area can behave differently during cutting, sewing, welding, filtration, or impregnation.
Ask which construction variables the supplier controls and how changes are authorized. For a coated fabric, relevant controls include substrate preparation, coating distribution, cure conditions, and adhesion. For a woven reinforcement, yarn alignment and construction stability affect handling and distortion. For filtration media, pore structure and treatment uniformity deserve attention alongside average permeability.
Performance requirements also interact. A heavier coating can improve resistance to liquid passage while reducing flexibility or vapor transport. A finish that changes surface energy can affect adhesive bonding. Assess these tradeoffs against the intended process rather than assuming that a higher individual value represents a better fabric.
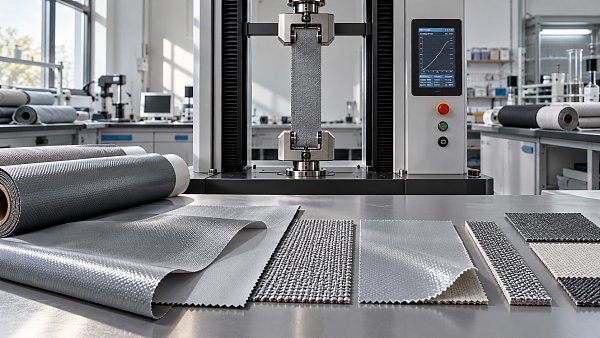
Use conversion trials to expose problems that flat laboratory specimens miss. Cutting can reveal fraying or coating damage; sewing introduces holes and local stresses; heat sealing tests the usable processing window. Reinforcement trials should include representative forming and resin contact. Record the processing settings so that a successful sample becomes a reproducible reference.
Look for consistency across the roll and across production lots
A supplier assessment should establish how variation is detected before shipment. Request results from multiple routine production lots where available, with enough context to identify changes in raw materials, equipment, or finishing conditions. Historical averages are less informative than records showing the spread of results and the handling of nonconforming production.
Variation has a physical location. Coating thickness can differ across the width; finishing conditions can drift along a roll. A specimen taken from one convenient location will not reveal every defect pattern. Agree on sampling locations that reflect the likely sources of variation, and distinguish qualification sampling from routine lot-release testing.
Visual grading and functional testing serve different purposes. A roll with few visible defects can still fail permeability or adhesion requirements. Conversely, an agreed cosmetic irregularity may have no effect on a hidden reinforcement application. Define defect categories, allowable frequency, and restrictions on usable areas in relation to the actual conversion process.
Request the documented response to an out-of-limit result. It should explain material segregation, investigation, retesting rules, disposition, and corrective action. Repeatedly testing until a passing result appears provides no reliable basis for release. Retesting needs a defined technical reason and a retained record of the original failure.
Audit the process controls that protect the specification
A facility assessment is most useful when it follows the proposed fabric through actual production. Establish which operations occur at the quoted site and which are subcontracted. Dyeing, coating, laminating, and specialist finishing can introduce variation outside the immediate fabric producer’s control.
Examine how production instructions connect to the approved specification. Controlled settings, material identification, equipment maintenance, and measuring-device calibration support repeatability. Their value becomes clearer when tied to a specific failure mechanism, such as uneven cure, excessive heat exposure, or incorrect treatment concentration.
Change control deserves explicit contractual treatment. Substituting a yarn source, coating formulation, finishing facility, or production route can alter performance while leaving the commercial grade name unchanged. Define which changes require notification, supporting evidence, or requalification before shipment. The approval process should also cover changes made by subcontractors.
A quality management certificate supports an assessment of organizational controls, but it does not certify every fabric property. Verify its scope, site coverage, validity, and relevance to the manufacturing activities being assessed. Product-specific evidence must still demonstrate conformity with the agreed requirements.
Make traceability and documentation usable at receipt
Traceability should connect a delivered roll to its production lot, relevant input materials, processing records, and release results. During qualification, select a sample roll identifier and ask for the associated records. This exercise shows whether the traceability system works beyond a written procedure.
Agree on the contents of shipment documentation. A certificate of analysis should identify the supplied grade and lot, the properties reported, the methods used, and whether values are actual lot results or typical data. A certificate of conformity generally serves a different purpose: it declares conformity without necessarily presenting measured results. Document titles alone do not establish their evidential value.
Regulatory and chemical declarations need a defined scope. Applicability depends on the destination market, intended use, material composition, and downstream product. Establish which substances or requirements are covered, whether the declaration applies to the finished fabric, and what supports it. A declaration for an untreated substrate does not establish the status of a subsequently applied coating.
Packaging requirements should preserve the approved condition. Specify roll identification, winding orientation, protection against moisture or contamination, and relevant storage limits. If shelf life affects coatings, finishes, or bonding performance, require a supported storage period and an identifiable starting date.
Use staged approval and a scorecard with firm gates
Move from document review to representative samples, conversion trials, and a controlled production order. Each stage should resolve a different uncertainty. Laboratory qualification establishes measured properties; conversion trials establish process compatibility; the initial production order tests whether routine manufacturing and shipment reproduce the approved material.
Set acceptance rules before scoring suppliers. Mandatory performance, material identity, and required documentation should operate as qualification gates. A weighted total must not allow strong delivery performance or a lower price to offset failure of a required protective property.
For suppliers that pass those gates, a scorecard can compare the remaining evidence:
- Technical fit: results obtained under comparable conditions, adequate margin against acceptance limits, and successful conversion at documented settings.
- Production consistency: variation across routine lots, sampling coverage, and evidence that corrective actions address recurring causes.
- Traceability and change control: the ability to retrieve roll-level records and identify changes that require renewed approval. Missing records should remain an unresolved issue rather than receiving an assumed passing score.
- Delivery and commercial execution: demonstrated lead-time reliability, agreed minimum quantities, usable roll dimensions, and clear responsibility for rejected material.
Distinguish evidence that was independently verified from supplier statements and information still awaiting confirmation. The scorecard should expose uncertainty rather than hide it inside a numerical total.
Record approval against the specific fabric grade, construction, finish, production site, and intended application. Define the events that trigger review, such as a material substitution, process transfer, repeated nonconformity, or changed service conditions. Subsequent orders can then be judged against a stable, documented basis for acceptance.
Recommended for You
 Smart MetersTamil Nadu Plans SIM-Based Upgrade for 17.7 Million Smart MetersTamil Nadu plans 17.7 million smart meters with proposed SIM-based upgrades. Explore potential supplier opportunities and the tender details still to come.By: Dr. Elena VoltNov 22, 2026
 Fiber LasersFiber Laser CE Marking: EU Safety Requirements and DocumentationFiber laser CE compliance goes beyond the mark. Explore EU safety requirements, essential documentation and practical checks before purchasing.By: Dr. Hideo TanakaNov 22, 2026
 Grid ResilienceUS Grid Equipment Shortages Could Hinder $1 Trillion UpgradeUS grid equipment shortages could hinder a $1 trillion upgrade. Explore how transformer supply, data centers and rising power demand could affect grid projects.By: Dr. Elena VoltNov 21, 2026
 Digital SeaChoosing Bluetooth Speakers: Sound Quality, Battery Life and PortabilityBluetooth speakers come in all shapes and sizes. Learn how to compare sound quality, battery life and portability to find the right fit for your listening needs.By: Captain Kenji SatoNov 21, 2026
 Subsea ROV/AUV2025 Ocean Equipment Report: China's Industry Moves Toward Scaled ApplicationChina's marine equipment industry is moving toward scaled application. Explore what the 2025 Ocean Equipment Report could mean for buyers, suppliers and offshore projects.By: Captain Kenji SatoNov 20, 2026
 Digital SeaChoosing a Thermoforming Vacuum Packaging Machine for Meat ProductsChoose a thermoforming vacuum packaging machine for meat with confidence. Compare sealing, film compatibility, hygiene and real-world production capacity.By: Captain Kenji SatoNov 20, 2026
 Digital SeaGreen Station Certification Cost: Fees and Budget ConsiderationsGreen station certification cost varies by scheme and site. Explore fees, hidden expenses, and budgeting tips to plan confidently and compare providers.By: Captain Kenji SatoNov 19, 2026
 UHV TransformersLIMiK Capital to Invest $328 Million in South Carolina Transformer PlantLIMiK Capital plans a $327.7 million transformer plant in South Carolina. Explore its potential impact on US grid supply and procurement.By: Dr. Elena VoltNov 18, 2026
 Digital SeaHow to Choose STEM Kits for Kids by Age, Interests, and Skill LevelChoose STEM kits that match your child's age, interests, and skills. Explore safety tips, project ideas, and practical checks to find an engaging fit.By: Captain Kenji SatoNov 18, 2026
 Digital SeaManufacturing Supplier Requirements: What to Include in Technical SpecificationsDiscover how manufacturing technical specifications and supplier requirements improve quality, simplify comparisons, and prevent delays with measurable acceptance criteria.By: Captain Kenji SatoNov 17, 2026
 Digital SeaChina's Environment Ministry Opens ALC Submarine Cable Project to ReviewChina's Environment Ministry opens the ALC submarine cable project's environmental assessment to review. Explore the proposed marine protection measures and what comes next.By: Captain Kenji SatoNov 16, 2026
 Precision LensesOptical Lens Surface Roughness Testing: Methods and Ra InterpretationOptical lens surface roughness testing explained: compare measurement methods, interpret Ra values, and define reliable acceptance criteria.By: Dr. Hideo TanakaNov 16, 2026
 Digital SeaBusiness Growth Strategies: How to Choose the Right Path for Your CompanyExplore business growth strategies and learn how to compare market opportunities, costs, risks, and capabilities to choose the right path for your company.By: Captain Kenji SatoNov 15, 2026
 Smart MetersIndia’s Competition Commission Approves Adani Acquisition of IntelliSmartExplore the reported CCI approval of Adani’s IntelliSmart acquisition and what a larger Indian smart meter platform could mean for suppliers and investors.By: Dr. Elena VoltNov 14, 2026
 Digital SeaHow Does a Ballast Cleaner Screening System Separate Track Ballast?Discover how a ballast cleaner screening system separates reusable stone from fines, what affects performance, and how to assess the results.By: Captain Kenji SatoNov 14, 2026
 Smart MetersPakistan to Seek World Bank and ADB Funding for Smart MetersPakistan seeks World Bank and ADB funding for smart meters on distribution transformers. Explore the plan to tackle power theft and improve grid efficiency.By: Dr. Elena VoltNov 13, 2026
 Digital SeaWhat Is Precision Medicine and How Does It Guide Treatment?Discover how precision medicine uses biomarkers and genetic insights to guide treatment, where it can help, and what to ask before testing.By: Captain Kenji SatoNov 13, 2026
 Grid Resilience2026 CSEE Annual Meeting Opens with Focus on AI and Power SystemsThe 2026 CSEE Annual Meeting explores AI, low-carbon power systems and ultra-high-voltage transmission. Discover why these discussions matter.By: Dr. Elena VoltNov 12, 2026
 Digital SeaShip Radar Detection Range: How Far Can It See and What Limits It?Ship radar detection range depends on more than the display scale. Discover how antenna height, weather, target size, and settings affect what radar can see.By: Captain Kenji SatoNov 12, 2026
 UHV TransformersGE Vernova to Invest $34.5 Million in Louisiana Transformer Plant ExpansionGE Vernova plans a $34.5 million transformer plant expansion in Louisiana. Explore its potential impact on North American supply and procurement.By: Dr. Elena VoltNov 11, 2026
 Digital SeaMetro Station Noise Criteria: Limits and Measurement MethodsExplore metro station noise criteria, applicable limits and measurement methods. Learn how to select metrics and assess compliance with confidence.By: Captain Kenji SatoNov 11, 2026
 Digital SeaKongsberg Maritime Unveils Arctic Hunter Unmanned Surface VesselKongsberg Maritime's Arctic Hunter unmanned surface vessel is proposed for the Royal Navy's Type 92 programme. Explore its technology and procurement implications.By: Captain Kenji SatoNov 10, 2026
 Sorting RobotsHow Accurate Is AI in Food Quality Control? Metrics and Testing MethodsExplore AI in food quality control accuracy, from recall and false negatives to validation methods. Learn how to assess real-world inspection reliability.By: Marcus SterlingNov 10, 2026
 UHV TransformersGE Vernova Selected for 6 GW HVDC Link in IndiaGE Vernova will design a 6 GW HVDC link for PGCIL, connecting Rajasthan and South Kalamb to support India's clean energy transition. Discover the project.By: Dr. Elena VoltNov 09, 2026
 Grid ResilienceEurope's Grid Compliance Standards in 2026: Generator Connection RequirementsExplore new grid compliance standards 2026 Europe projects must address, from generator connection rules to testing and documentation. Prepare for approval.By: Dr. Elena VoltNov 09, 2026
 Technical FabricsNonwoven Bonding Cost Data: Comparing Thermal and Chemical ProcessesExplore nonwoven bonding cost data to compare thermal and chemical processes, assess usable yield, and choose the best-value option for your application.By: Chloe DuboisNov 08, 2026
 Fiber LasersIndustrial Lasers to 2035: Automotive Lightweighting and Precision Welding Drive DemandExplore the industrial laser market outlook to 2035 and discover how automotive lightweighting and precision welding could shape demand and procurement.By: Dr. Hideo TanakaNov 07, 2026
 Technical FabricsChoosing Geotextile Under Railway Ballast: Key Performance RequirementsChoosing geotextile under railway ballast? Explore essential filtration, drainage, strength and durability criteria to make a confident, project-specific selection.By: Chloe DuboisNov 07, 2026
 Digital SeaChoosing Rail Welding Equipment for Maintenance: Field Conditions and Weld TypesChoose rail welding equipment for maintenance with confidence. Compare welding methods, field constraints, inspection needs, and lifecycle costs.By: Captain Kenji SatoNov 06, 2026
 Digital SeaIndia Broadband Forum Urges Stronger Submarine Cable ResilienceIndia’s submarine cable resilience is in focus as the Broadband India Forum urges faster repairs, more vessels and stronger landing infrastructure.By: Captain Kenji SatoNov 06, 2026
 Digital SeaChoosing a Railway Network Switch Supplier: Reliability and Support CriteriaChoosing a railway network switch supplier? Compare reliability, standards evidence, cybersecurity, and lifecycle support to reduce project risk.By: Captain Kenji SatoNov 05, 2026