BDI: 1,842 ▼ 1.2%
COTTON NO.2: 84.12 ▲ 0.4%
LME COPPER: 8,432.50 ▲ 2.1%
FOOD SAFETY INDEX: 94.2 ARCHIVE_SECURED
OPTICAL INDEX: 11,204.09 STABLE
BDI: 1,842 ▼ 1.2%
SECTOR INDEX
V.24.08 ARCHIVE
Hot Articles
- Tamil Nadu Plans SIM-Based Upgrade for 17.7 Million Smart MetersTamil Nadu plans 17.7 million smart meters with proposed SIM-based upgrades. Explore potential supplier opportunities and the tender details still to come.
- Fiber Laser CE Marking: EU Safety Requirements and DocumentationFiber laser CE compliance goes beyond the mark. Explore EU safety requirements, essential documentation and practical checks before purchasing.
- US Grid Equipment Shortages Could Hinder $1 Trillion UpgradeUS grid equipment shortages could hinder a $1 trillion upgrade. Explore how transformer supply, data centers and rising power demand could affect grid projects.
Optical Lens Surface Roughness Testing: Methods and Ra Interpretation


Optical lens surface roughness testing produces a meaningful Ra value only when the measured surface, spatial bandwidth, filtering, and evaluation length are defined. Two results expressed in nanometres are not necessarily comparable: a short scan across a polished patch and a longer scan that includes broader surface structure can produce different values on the same lens. Acceptance therefore depends on the complete measurement definition, not on Ra alone.
For a technical specification, identify the relevant optical surface and measurement region, the profile or area method, the processing applied to the data, and the required reporting conditions. Surface texture standards provide terminology and measurement frameworks, but a reference to a standard does not by itself establish a suitable roughness limit for every lens.
What Ra describes on a lens surface
Ra is the arithmetic mean of the absolute height deviations of a roughness profile from its mean line over the evaluation length. In practical terms, it indicates the average magnitude of the profile’s departures from that line after the specified processing. It does not preserve the sign of those departures, and it does not describe their arrangement along the surface.
A profile with shallow, closely spaced polishing marks can have the same Ra as one containing a smaller number of deeper features. Their optical effects can differ because scatter depends on feature size, direction, surface material, wavelength, and illumination geometry. Ra also does not identify whether a prominent feature is a scratch, a pit, contamination, or a measurement artifact.
The distinction between Ra and Sa matters. Ra is calculated from a line profile; Sa is an arithmetic mean height parameter calculated over an area. Both are commonly reported in length units, but their different sampling geometries mean that their numerical values should not be substituted without an agreed method. A line can miss an isolated defect that appears in an area scan, while the area result depends on the field of view and data processing.
Selecting a measurement method
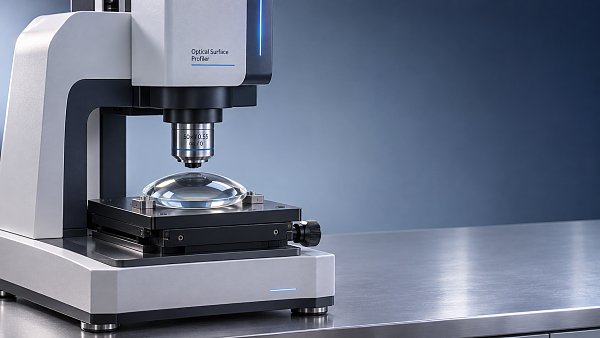
Contact and optical instruments each sample the surface through a measurement system with finite resolution and a defined response to surface slope. The choice should follow the lens geometry, material, expected texture, and need to preserve the finished surface.
A stylus trace requires particular care on a finished lens. A finite-radius tip cannot enter every narrow valley, so the recorded profile represents the surface as sampled by the tip. Excessive force or repeated tracing can damage a coating or alter a soft surface. A trace across a steeply curved region also places demands on instrument travel and slope capability. When contact is permissible, trace orientation should be recorded relative to visible polishing or machining marks.
Optical techniques avoid stylus contact, but a height map is still a reconstruction from an optical signal. Weak reflections, steep local slopes, transparent layers, and surfaces near the edge of an objective’s working range can produce invalid pixels or misleading heights. On a coated lens, reflections from different interfaces can affect the signal; the measured interface and any coating-related limitations should be established before comparing results with a substrate specification.
Atomic force microscopy offers a closer view of fine texture, yet its small scan area creates a sampling problem. A smooth patch does not establish that the full clear aperture has the same finish. Larger-area measurements and multiple selected locations are often needed when uniformity across the lens matters.
Separate surface texture from lens shape
A lens is intentionally curved. The raw measurement therefore includes nominal shape as well as departures from that shape. Tilt and an appropriate form model are commonly removed before roughness is calculated. The choice of model matters: removing too little form leaves curvature in the residual profile, while removing an overly flexible fitted surface can suppress real long-wavelength structure.
Roughness filtering then separates the reported profile from longer-wavelength components according to the specified filter and cutoff. The cutoff is a spatial scale, not a universal dividing line between good and bad surface features. Changing it changes which features contribute to Ra. Short-wavelength response also matters: instrument resolution, stylus tip geometry, optical configuration, sampling interval, and any short-wavelength filtering determine how much fine texture enters the result.
For example, two measurements from the same polished glass region can disagree because one retains broader polishing structure that the other removes. That discrepancy does not automatically establish that either instrument is inaccurate. First compare the form removal, filter type and settings, sampling interval, trace length, and measurement location. Agreement in units alone is insufficient.
Edge handling deserves attention on small lenses. Filtering near the ends of a profile can be affected by limited data outside the evaluation region. Measurements close to a bevel or aperture boundary can also include edge artifacts or material outside the specified optical zone. The report should distinguish the recorded trace or image size from the portion actually used to calculate the parameter.
Match the sampling plan to the surface and optical function
A single central measurement is convenient, but it may not represent a lens polished with a process that varies from centre to edge. Define positions within the clear aperture and record their distances or coordinates relative to the lens centre. For aspheric surfaces, include local slope and measurement accessibility when choosing locations. If different zones have different functional requirements, assign and report their results separately.
Direction is equally consequential. A line scan parallel to polishing marks can cross fewer height changes than a perpendicular scan. When texture has a preferred direction, use defined orientations or acquire an area map that reveals the pattern. Multiple traces also make it easier to distinguish a repeatable texture from a single local event.
Preparation should preserve the surface being evaluated. Loose particles, cleaning residue, fingerprints, and moisture can produce apparent peaks or interrupt an optical signal. Use a cleaning procedure compatible with the substrate and coating, and document it when the result is sensitive to preparation. If a feature disappears after permitted cleaning, the first measurement represented the surface condition at that time; it should not silently be treated as permanent substrate roughness.
Inspect invalid or missing data before accepting an area parameter. Interpolating across a small isolated gap and reconstructing a substantial unmeasured region are different operations. Report the extent and treatment of missing data, and avoid comparing a heavily reconstructed map with a complete map as though they sampled the same surface.
Interpreting Ra alongside optical performance
For smooth optical surfaces, roughness is often considered because surface irregularities scatter light. The relationship is governed by the height and spatial distribution of features as well as wavelength and measurement geometry. A low Ra does not guarantee low scatter at every angle, and an Ra limit chosen without the relevant spatial scales may fail to control the structure that matters in the optical system.
A power spectral density description can add detail by showing how surface variation is distributed across spatial frequencies. It is useful when two surfaces have similar Ra values but different polishing textures, or when a scattering model specifies a spatial-frequency range. The result still requires a stated measurement bandwidth and processing method; an instrument cannot describe frequencies it has not resolved or sampled.
Isolated scratches and digs require separate consideration. Averaging over a long profile or large area can dilute the contribution of a localized defect, while a trace that happens to cross it can produce a markedly higher value. Where local defects affect imaging, coating integrity, or scatter, evaluate them under an appropriate surface-imperfection specification rather than relying on Ra as their sole acceptance measure.
Likewise, surface roughness does not replace a form or wavefront measurement. A lens can have a smooth local finish and still depart from its intended shape. Conversely, a satisfactory form result does not establish that fine-scale texture meets a scatter-sensitive requirement. The relevant specifications should identify the scale and optical effect each measurement is intended to control.
Make reported results comparable
A useful test report ties the numerical result to a reproducible measurement. It identifies the surface and coating condition, instrument and measurement mode, locations and orientations, profile length or area dimensions, sampling, form removal, filters, parameter units, and number of measurements. It also states whether the reported value is an individual result, an average, or the highest value among defined locations. An average can conceal a local failure if the acceptance rule applies to each location.
Measurement uncertainty becomes especially important when a result lies near a limit. Calibration or verification of the instrument, repeatability, environmental conditions, data processing, and surface variability all contribute to confidence in the comparison. The acceptance agreement should state how uncertainty is handled; a bare value rounded to a few digits does not resolve a borderline result.
When results from different instruments disagree, return to the original profiles or height maps where available. Compare measured regions, resolved spatial scales, filtering, and data quality before attributing the difference to a change in the lens. A shared test definition and an agreed acceptance rule make subsequent measurements more useful than an Ra value detached from its conditions.
Recommended for You
 Smart MetersTamil Nadu Plans SIM-Based Upgrade for 17.7 Million Smart MetersTamil Nadu plans 17.7 million smart meters with proposed SIM-based upgrades. Explore potential supplier opportunities and the tender details still to come.By: Dr. Elena VoltNov 22, 2026
 Fiber LasersFiber Laser CE Marking: EU Safety Requirements and DocumentationFiber laser CE compliance goes beyond the mark. Explore EU safety requirements, essential documentation and practical checks before purchasing.By: Dr. Hideo TanakaNov 22, 2026
 Grid ResilienceUS Grid Equipment Shortages Could Hinder $1 Trillion UpgradeUS grid equipment shortages could hinder a $1 trillion upgrade. Explore how transformer supply, data centers and rising power demand could affect grid projects.By: Dr. Elena VoltNov 21, 2026
 Digital SeaChoosing Bluetooth Speakers: Sound Quality, Battery Life and PortabilityBluetooth speakers come in all shapes and sizes. Learn how to compare sound quality, battery life and portability to find the right fit for your listening needs.By: Captain Kenji SatoNov 21, 2026
 Subsea ROV/AUV2025 Ocean Equipment Report: China's Industry Moves Toward Scaled ApplicationChina's marine equipment industry is moving toward scaled application. Explore what the 2025 Ocean Equipment Report could mean for buyers, suppliers and offshore projects.By: Captain Kenji SatoNov 20, 2026
 Digital SeaChoosing a Thermoforming Vacuum Packaging Machine for Meat ProductsChoose a thermoforming vacuum packaging machine for meat with confidence. Compare sealing, film compatibility, hygiene and real-world production capacity.By: Captain Kenji SatoNov 20, 2026
 Digital SeaGreen Station Certification Cost: Fees and Budget ConsiderationsGreen station certification cost varies by scheme and site. Explore fees, hidden expenses, and budgeting tips to plan confidently and compare providers.By: Captain Kenji SatoNov 19, 2026
 UHV TransformersLIMiK Capital to Invest $328 Million in South Carolina Transformer PlantLIMiK Capital plans a $327.7 million transformer plant in South Carolina. Explore its potential impact on US grid supply and procurement.By: Dr. Elena VoltNov 18, 2026
 Digital SeaHow to Choose STEM Kits for Kids by Age, Interests, and Skill LevelChoose STEM kits that match your child's age, interests, and skills. Explore safety tips, project ideas, and practical checks to find an engaging fit.By: Captain Kenji SatoNov 18, 2026
 Digital SeaManufacturing Supplier Requirements: What to Include in Technical SpecificationsDiscover how manufacturing technical specifications and supplier requirements improve quality, simplify comparisons, and prevent delays with measurable acceptance criteria.By: Captain Kenji SatoNov 17, 2026
 Digital SeaChina's Environment Ministry Opens ALC Submarine Cable Project to ReviewChina's Environment Ministry opens the ALC submarine cable project's environmental assessment to review. Explore the proposed marine protection measures and what comes next.By: Captain Kenji SatoNov 16, 2026
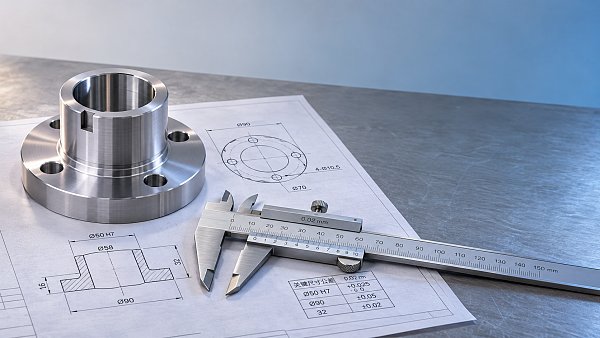
 Precision LensesOptical Lens Surface Roughness Testing: Methods and Ra InterpretationOptical lens surface roughness testing explained: compare measurement methods, interpret Ra values, and define reliable acceptance criteria.By: Dr. Hideo TanakaNov 16, 2026
 Digital SeaBusiness Growth Strategies: How to Choose the Right Path for Your CompanyExplore business growth strategies and learn how to compare market opportunities, costs, risks, and capabilities to choose the right path for your company.By: Captain Kenji SatoNov 15, 2026
 Smart MetersIndia’s Competition Commission Approves Adani Acquisition of IntelliSmartExplore the reported CCI approval of Adani’s IntelliSmart acquisition and what a larger Indian smart meter platform could mean for suppliers and investors.By: Dr. Elena VoltNov 14, 2026
 Digital SeaHow Does a Ballast Cleaner Screening System Separate Track Ballast?Discover how a ballast cleaner screening system separates reusable stone from fines, what affects performance, and how to assess the results.By: Captain Kenji SatoNov 14, 2026
 Smart MetersPakistan to Seek World Bank and ADB Funding for Smart MetersPakistan seeks World Bank and ADB funding for smart meters on distribution transformers. Explore the plan to tackle power theft and improve grid efficiency.By: Dr. Elena VoltNov 13, 2026
 Digital SeaWhat Is Precision Medicine and How Does It Guide Treatment?Discover how precision medicine uses biomarkers and genetic insights to guide treatment, where it can help, and what to ask before testing.By: Captain Kenji SatoNov 13, 2026
 Grid Resilience2026 CSEE Annual Meeting Opens with Focus on AI and Power SystemsThe 2026 CSEE Annual Meeting explores AI, low-carbon power systems and ultra-high-voltage transmission. Discover why these discussions matter.By: Dr. Elena VoltNov 12, 2026
 Digital SeaShip Radar Detection Range: How Far Can It See and What Limits It?Ship radar detection range depends on more than the display scale. Discover how antenna height, weather, target size, and settings affect what radar can see.By: Captain Kenji SatoNov 12, 2026
 UHV TransformersGE Vernova to Invest $34.5 Million in Louisiana Transformer Plant ExpansionGE Vernova plans a $34.5 million transformer plant expansion in Louisiana. Explore its potential impact on North American supply and procurement.By: Dr. Elena VoltNov 11, 2026
 Digital SeaMetro Station Noise Criteria: Limits and Measurement MethodsExplore metro station noise criteria, applicable limits and measurement methods. Learn how to select metrics and assess compliance with confidence.By: Captain Kenji SatoNov 11, 2026
 Digital SeaKongsberg Maritime Unveils Arctic Hunter Unmanned Surface VesselKongsberg Maritime's Arctic Hunter unmanned surface vessel is proposed for the Royal Navy's Type 92 programme. Explore its technology and procurement implications.By: Captain Kenji SatoNov 10, 2026
 Sorting RobotsHow Accurate Is AI in Food Quality Control? Metrics and Testing MethodsExplore AI in food quality control accuracy, from recall and false negatives to validation methods. Learn how to assess real-world inspection reliability.By: Marcus SterlingNov 10, 2026
 UHV TransformersGE Vernova Selected for 6 GW HVDC Link in IndiaGE Vernova will design a 6 GW HVDC link for PGCIL, connecting Rajasthan and South Kalamb to support India's clean energy transition. Discover the project.By: Dr. Elena VoltNov 09, 2026
 Grid ResilienceEurope's Grid Compliance Standards in 2026: Generator Connection RequirementsExplore new grid compliance standards 2026 Europe projects must address, from generator connection rules to testing and documentation. Prepare for approval.By: Dr. Elena VoltNov 09, 2026
 Technical FabricsNonwoven Bonding Cost Data: Comparing Thermal and Chemical ProcessesExplore nonwoven bonding cost data to compare thermal and chemical processes, assess usable yield, and choose the best-value option for your application.By: Chloe DuboisNov 08, 2026
 Fiber LasersIndustrial Lasers to 2035: Automotive Lightweighting and Precision Welding Drive DemandExplore the industrial laser market outlook to 2035 and discover how automotive lightweighting and precision welding could shape demand and procurement.By: Dr. Hideo TanakaNov 07, 2026
 Technical FabricsChoosing Geotextile Under Railway Ballast: Key Performance RequirementsChoosing geotextile under railway ballast? Explore essential filtration, drainage, strength and durability criteria to make a confident, project-specific selection.By: Chloe DuboisNov 07, 2026
 Digital SeaChoosing Rail Welding Equipment for Maintenance: Field Conditions and Weld TypesChoose rail welding equipment for maintenance with confidence. Compare welding methods, field constraints, inspection needs, and lifecycle costs.By: Captain Kenji SatoNov 06, 2026
 Digital SeaIndia Broadband Forum Urges Stronger Submarine Cable ResilienceIndia’s submarine cable resilience is in focus as the Broadband India Forum urges faster repairs, more vessels and stronger landing infrastructure.By: Captain Kenji SatoNov 06, 2026
 Digital SeaChoosing a Railway Network Switch Supplier: Reliability and Support CriteriaChoosing a railway network switch supplier? Compare reliability, standards evidence, cybersecurity, and lifecycle support to reduce project risk.By: Captain Kenji SatoNov 05, 2026