BDI: 1,842 ▼ 1.2%
COTTON NO.2: 84.12 ▲ 0.4%
LME COPPER: 8,432.50 ▲ 2.1%
FOOD SAFETY INDEX: 94.2 ARCHIVE_SECURED
OPTICAL INDEX: 11,204.09 STABLE
BDI: 1,842 ▼ 1.2%
SECTOR INDEX
V.24.08 ARCHIVE
Hot Articles
- How Does a Ballast Cleaner Screening System Separate Track Ballast?Discover how a ballast cleaner screening system separates reusable stone from fines, what affects performance, and how to assess the results.
- Pakistan to Seek World Bank and ADB Funding for Smart MetersPakistan seeks World Bank and ADB funding for smart meters on distribution transformers. Explore the plan to tackle power theft and improve grid efficiency.
- What Is Precision Medicine and How Does It Guide Treatment?Discover how precision medicine uses biomarkers and genetic insights to guide treatment, where it can help, and what to ask before testing.
When Should Semiconductor Equipment Be Refurbished Rather Than Replaced?


When should semiconductor equipment be refurbished instead of replaced? The practical answer is: when the tool’s core platform remains mechanically sound and process-capable, while its limitations can be corrected through targeted restoration, modernization, and requalification at a lower total risk than buying new.
That sounds straightforward, but the decision is rarely driven by machine age alone. A 15-year-old deposition, etch, metrology, or wafer-handling tool may still be a dependable production asset if its chamber integrity, motion systems, utilities, and process window can be recovered. Conversely, a newer system may be a poor refurbishment candidate if the OEM has withdrawn support, critical parts are unavailable, or its architecture cannot meet current device requirements.
For fab managers, procurement directors, equipment engineers, and global distributors, the real question is not “old versus new.” It is whether the asset can return to stable, documented, commercially sensible operation without introducing unacceptable yield, safety, compliance, or delivery risk.
Refurbishment makes sense when the process platform is still relevant
The strongest reason to refurbish is that the equipment still supports the product roadmap. This is particularly common in mature-node manufacturing, discrete devices, power semiconductors, MEMS, sensors, optoelectronics, compound semiconductors, and specialized packaging lines. These operations may not require the newest process node, but they still require repeatable film quality, clean handling, thermal control, alignment accuracy, and uptime.
If a tool can meet current specifications—or can do so after a defined upgrade—it may have substantial remaining economic life. The underlying frame, vacuum chamber, process modules, and wafer transport architecture often retain value long after controllers, sensors, pumps, software interfaces, and safety components become dated.
In this situation, replacement can be unnecessarily disruptive. A new machine may require facility modifications, recipe redevelopment, operator retraining, qualification wafers, customer approvals, and lengthy ramp-up work. Refurbishment is often the more measured choice when continuity matters as much as technical improvement.
Look beyond the purchase price: compare lifecycle outcomes
A replacement decision can appear obvious when repair invoices begin to rise. Yet a high recent maintenance cost does not automatically mean that a tool should be retired. The more useful comparison is between the full lifecycle cost of refurbishment and the full operational cost of replacement.
A credible refurbishment business case should include the scope of restoration, replacement parts, controls upgrades, installation, qualification, expected downtime, training, consumables, service coverage, and the likely remaining service life. The replacement scenario should include not only the acquisition price, but also lead time, import or logistics exposure, cleanroom integration, utilities work, process transfer, acceptance testing, and production losses during transition.
For many manufacturers, especially those operating mixed-vintage fleets, the critical value lies in avoiding a long capacity gap. A refurbished tool that returns to qualified output within a manageable schedule may protect revenue and customer commitments more effectively than a replacement tool with an uncertain delivery date.
There is also a portfolio question. A new platform may be justified for a high-volume bottleneck process, while refurbishment is more sensible for backup capacity, engineering lots, lower-volume product families, or a stable legacy line. Asset strategy does not need to impose one answer across every toolset.
Signs that a tool is a good refurbishment candidate
Equipment engineers commonly look for a combination of favorable conditions rather than one decisive indicator. A tool is usually worth deeper evaluation when most of the following are true:
- The mechanical structure is sound. Major frames, chambers, robotics, load locks, stages, and utility interfaces are not showing irrecoverable wear, corrosion, distortion, or repeated structural failures.
- Process performance is understood. Historical data exists for yield, repeatability, defectivity, throughput, and maintenance events. A known performance baseline is much easier to restore than an undocumented tool with unexplained variation.
- Critical assemblies can be sourced or rebuilt. This may include vacuum components, mass-flow controllers, RF systems, power supplies, motion hardware, optics, temperature-control parts, and electronics.
- Obsolescence is concentrated rather than systemic. Replacing an aging PLC, HMI, motion controller, or safety circuit is different from confronting a platform where every proprietary subsystem has reached end-of-life.
- The process can be requalified realistically. The fab has recipes, reference wafers, metrology methods, engineering time, and customer approval pathways needed to validate the restored system.
- Facility compatibility remains intact. The tool still fits available power, gases, exhaust, chilled water, clean dry air, abatement, and cleanroom space without costly reconstruction.
These indicators are not a substitute for engineering review. They do, however, separate an asset with recoverable value from one that may only look economical before hidden risks emerge.
What a serious refurbishment should include
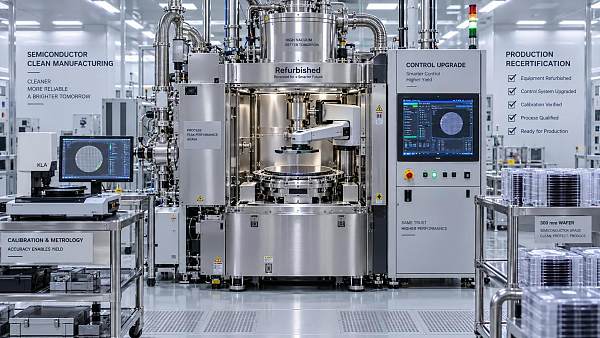
Refurbishment is sometimes confused with cosmetic cleaning and basic repair. In semiconductor production, that approach is rarely enough. A meaningful project begins with an incoming condition assessment: equipment history, fault records, configuration verification, contamination review, subsystem inspection, and identification of obsolete or high-risk components.
The scope should then distinguish between restoration and modernization. Restoration returns the system to its intended operating condition through cleaning, rebuilding, replacement of worn components, leak checking, calibration, and functional testing. Modernization addresses the elements that make the tool difficult or unsafe to operate today, such as unsupported controls, limited data capture, outdated interlocks, poor remote diagnostics, or incompatible communication protocols.
For process equipment, the final stage is not merely “power on.” It should involve factory acceptance testing where feasible, installation checks, utility verification, baseline characterization, recipe validation, and documented performance qualification. Depending on the application, this may include particle monitoring, vacuum integrity testing, film uniformity, critical-dimension repeatability, temperature stability, alignment accuracy, or wafer-handling repeatability.
A refurbishment provider should be able to explain what is being changed, why it is being changed, and how each modification may affect process behavior. Vague assurances are not enough when a tool sits inside a yield-sensitive production flow.
Replacement is the better choice when risk cannot be engineered out
There are clear cases where replacement is the more responsible decision. If the equipment cannot meet required accuracy, contamination, throughput, overlay, defect-density, or traceability targets even after reasonable upgrades, continuing to invest in it can become a false economy.
The same applies when a tool has fundamental safety deficiencies. Legacy electrical systems, inadequate guarding, obsolete emergency-stop architecture, unmanaged chemical risks, or unreliable interlocks may create exposures that are difficult to justify. Compliance requirements vary by region and site, but safety modernization must be assessed as a design issue—not treated as a paperwork exercise.
Replacement should also be considered when proprietary components are no longer obtainable and cannot be reverse-engineered or substituted without compromising reliability. A tool that depends on one fragile source for a discontinued board, controller, or process-critical assembly can become a production liability. The problem is not only the next failure; it is the uncertainty surrounding every future failure.
Finally, replacement may be necessary when the business itself has changed. A factory moving to higher wafer sizes, new materials, stricter traceability, automated material handling, or advanced process control may need a platform designed for that environment. Retrofitting a legacy machine beyond its original architecture can cost more, take longer, and deliver less certainty than acquiring the right system.
Do not underestimate controls, software, and data integration
Modern semiconductor equipment is judged not only by what happens inside the chamber or at the stage. It is also judged by how reliably the tool communicates. Factories increasingly need equipment status, alarms, recipe governance, maintenance records, and traceability data to move through MES, SPC, and quality systems.
That makes controls retrofits one of the most valuable refurbishment pathways. Updating legacy controllers, industrial PCs, HMI screens, network interfaces, and data logging can improve maintainability without altering the core process hardware. However, the work must be carefully governed. Changes to control logic, timing, sensor scaling, or motion profiles can affect process output in subtle ways.
A good rule is to define what must remain functionally equivalent and what should be improved. Preserve validated process behavior where possible; modernize reliability, diagnostics, cybersecurity posture, safety monitoring, and data accessibility where the business needs it. Documentation, version control, backup procedures, and operator training are part of the technical deliverable.
A practical decision sequence for procurement and engineering teams
Before issuing a purchase order for either refurbishment or replacement, bring operations, process engineering, maintenance, EHS, quality, and procurement into the same review. Each group sees a different risk: production sees downtime, engineering sees process drift, maintenance sees parts exposure, quality sees qualification burden, and procurement sees cost and supplier continuity.
- Define the required output. Establish the actual requirements for throughput, yield, process capability, data connectivity, safety, and expected operating horizon.
- Assess the installed tool condition. Inspect high-risk subsystems and review failure history rather than relying on age or visual condition.
- Map the upgrade path. Identify which components can be restored, replaced, upgraded, or supported over time.
- Model downtime and qualification. Compare realistic production interruption, not idealized project schedules.
- Compare total risk-adjusted cost. Include likely contingencies, spare-parts strategy, service response, and residual value.
- Set acceptance criteria before work begins. Agree on measurable functional, process, safety, and documentation requirements.
This sequence is especially important in cross-border procurement, where equipment transport, export controls, local electrical standards, spare-parts customs clearance, and service access can all affect the final result.
Frequently asked questions
Is refurbished semiconductor equipment reliable enough for production?
It can be, provided the refurbishment scope is tied to documented condition assessment and requalification. Reliability depends on the quality of rebuilt subsystems, availability of critical spares, calibration, process validation, and ongoing maintenance discipline. A refurbished tool should be evaluated as a controlled engineering asset, not as a bargain purchase.
How old is too old to refurbish semiconductor equipment?
There is no universal age limit. Some older tools remain valuable because their mechanical platforms are robust and their processes are still commercially relevant. Others become unsuitable much earlier because of unsupported electronics, poor parts availability, changing safety expectations, or inability to meet process requirements. Technology relevance and supportability matter more than the manufacturing date.
Can refurbishment improve tool performance?
Yes, particularly when the project includes replacement of degraded components, upgraded controls, improved sensing, refreshed vacuum or thermal systems, and better diagnostics. Still, improvements should be defined and tested carefully. Refurbishment can restore or enhance practical performance, but it cannot erase the physical limits of the original architecture.
What documentation should buyers request?
Request the equipment configuration, condition report, list of replaced and upgraded components, calibration records, test results, software and controller versions, wiring or pneumatic updates, safety-related changes, spare-parts recommendations, and acceptance criteria. For process-critical equipment, include the agreed qualification plan and any available baseline data.
The decision is about fit, not sentiment
Semiconductor equipment is often treated as either a depreciating asset to be discarded or a legacy machine to be kept alive indefinitely. Both views can lead to poor decisions. The better approach is evidence-based: retain and refurbish equipment when its core platform, process role, and support path remain credible; replace it when technical, compliance, or supply-chain risks exceed what a disciplined upgrade can solve.
For organizations comparing equipment across advanced manufacturing environments, this is where structured benchmarking matters. G-MCE’s cross-disciplinary perspective—linking technical standards, asset lifecycle considerations, supply-chain visibility, and industrial risk—supports a more complete conversation than a simple quote comparison. The objective is not to preserve old equipment at all costs. It is to choose the asset path that keeps production stable, traceable, and economically defensible.
Recommended for You
 Digital SeaHow Does a Ballast Cleaner Screening System Separate Track Ballast?Discover how a ballast cleaner screening system separates reusable stone from fines, what affects performance, and how to assess the results.By: Captain Kenji SatoNov 14, 2026
 Smart MetersPakistan to Seek World Bank and ADB Funding for Smart MetersPakistan seeks World Bank and ADB funding for smart meters on distribution transformers. Explore the plan to tackle power theft and improve grid efficiency.By: Dr. Elena VoltNov 13, 2026
 Digital SeaWhat Is Precision Medicine and How Does It Guide Treatment?Discover how precision medicine uses biomarkers and genetic insights to guide treatment, where it can help, and what to ask before testing.By: Captain Kenji SatoNov 13, 2026
 Grid Resilience2026 CSEE Annual Meeting Opens with Focus on AI and Power SystemsThe 2026 CSEE Annual Meeting explores AI, low-carbon power systems and ultra-high-voltage transmission. Discover why these discussions matter.By: Dr. Elena VoltNov 12, 2026
 Digital SeaShip Radar Detection Range: How Far Can It See and What Limits It?Ship radar detection range depends on more than the display scale. Discover how antenna height, weather, target size, and settings affect what radar can see.By: Captain Kenji SatoNov 12, 2026
 UHV TransformersGE Vernova to Invest $34.5 Million in Louisiana Transformer Plant ExpansionGE Vernova plans a $34.5 million transformer plant expansion in Louisiana. Explore its potential impact on North American supply and procurement.By: Dr. Elena VoltNov 11, 2026
 Digital SeaMetro Station Noise Criteria: Limits and Measurement MethodsExplore metro station noise criteria, applicable limits and measurement methods. Learn how to select metrics and assess compliance with confidence.By: Captain Kenji SatoNov 11, 2026
 Digital SeaKongsberg Maritime Unveils Arctic Hunter Unmanned Surface VesselKongsberg Maritime's Arctic Hunter unmanned surface vessel is proposed for the Royal Navy's Type 92 programme. Explore its technology and procurement implications.By: Captain Kenji SatoNov 10, 2026
 Sorting RobotsHow Accurate Is AI in Food Quality Control? Metrics and Testing MethodsExplore AI in food quality control accuracy, from recall and false negatives to validation methods. Learn how to assess real-world inspection reliability.By: Marcus SterlingNov 10, 2026
 UHV TransformersGE Vernova Selected for 6 GW HVDC Link in IndiaGE Vernova will design a 6 GW HVDC link for PGCIL, connecting Rajasthan and South Kalamb to support India's clean energy transition. Discover the project.By: Dr. Elena VoltNov 09, 2026
 Grid ResilienceEurope's Grid Compliance Standards in 2026: Generator Connection RequirementsExplore new grid compliance standards 2026 Europe projects must address, from generator connection rules to testing and documentation. Prepare for approval.By: Dr. Elena VoltNov 09, 2026
 Technical FabricsNonwoven Bonding Cost Data: Comparing Thermal and Chemical ProcessesExplore nonwoven bonding cost data to compare thermal and chemical processes, assess usable yield, and choose the best-value option for your application.By: Chloe DuboisNov 08, 2026
 Fiber LasersIndustrial Lasers to 2035: Automotive Lightweighting and Precision Welding Drive DemandExplore the industrial laser market outlook to 2035 and discover how automotive lightweighting and precision welding could shape demand and procurement.By: Dr. Hideo TanakaNov 07, 2026
 Technical FabricsChoosing Geotextile Under Railway Ballast: Key Performance RequirementsChoosing geotextile under railway ballast? Explore essential filtration, drainage, strength and durability criteria to make a confident, project-specific selection.By: Chloe DuboisNov 07, 2026
 Digital SeaChoosing Rail Welding Equipment for Maintenance: Field Conditions and Weld TypesChoose rail welding equipment for maintenance with confidence. Compare welding methods, field constraints, inspection needs, and lifecycle costs.By: Captain Kenji SatoNov 06, 2026
 Digital SeaIndia Broadband Forum Urges Stronger Submarine Cable ResilienceIndia’s submarine cable resilience is in focus as the Broadband India Forum urges faster repairs, more vessels and stronger landing infrastructure.By: Captain Kenji SatoNov 06, 2026
 Digital SeaChoosing a Railway Network Switch Supplier: Reliability and Support CriteriaChoosing a railway network switch supplier? Compare reliability, standards evidence, cybersecurity, and lifecycle support to reduce project risk.By: Captain Kenji SatoNov 05, 2026
 Grid ResilienceUS Grid Equipment Import Ban Raises Cost and Implementation ConcernsThe US grid equipment import ban raises concerns over costs and delivery delays. Explore how unclear criteria could affect procurement and supply chains.By: Dr. Elena VoltNov 05, 2026
 Digital SeaRailway Coupler Price: How Type and Specifications Affect QuotesRailway coupler price depends on type, specifications, and order scope. Learn how to compare quotes, avoid hidden costs, and make a confident buying decision.By: Captain Kenji SatoNov 04, 2026
 Grid ResilienceGlobal Smart Grid Companies Raise $3 Billion in First Nine Months of 2026Global smart grid companies raised $3 billion in the first nine months of 2026. Explore the funding breakdown and potential implications for buyers and suppliers.By: Dr. Elena VoltNov 04, 2026
 Digital SeaChoosing Wholesale Pet Toys: How to Evaluate Suppliers and Minimum OrdersWholesale pet toys: learn how to assess suppliers, compare minimum orders and landed costs, and reduce inventory risk before you buy.By: Captain Kenji SatoNov 03, 2026
 Digital SeaSustainable Packaging Design: How to Choose Materials and Reduce WasteDiscover how sustainable packaging design helps reduce waste, protect products, and control costs with practical material choices and proven testing strategies.By: Captain Kenji SatoNov 02, 2026
 Technical FabricsUSMCA's First Joint Review Puts Textile Supply Chain Rules in FocusUSMCA's first joint review puts textile supply chain rules in focus. Explore potential impacts on origin compliance, sourcing and tariff treatment.By: Chloe DuboisNov 02, 2026
 Digital SeaManufacturing KPI Benchmarking: How to Compare Production PerformanceBenchmarking KPI manufacturing performance? Learn how to compare OEE, quality and downtime, identify meaningful gaps, and turn insights into practical improvements.By: Captain Kenji SatoNov 01, 2026
 Smart MetersCCI Approves Adani Energy Solutions' ₹305 Billion Acquisition of IntelliSmartCCI approves Adani Energy Solutions' ₹305 billion acquisition of IntelliSmart. Discover what the deal could mean for India's smart meter market.By: Dr. Elena VoltNov 01, 2026
 Digital SeaChoosing a Coin Laundry Machinery OEM: What Buyers Should EvaluateChoosing a coin laundry machinery OEM? Compare machine specifications, payment integration, lifecycle costs, and support to make a confident buying decision.By: Captain Kenji SatoOct 31, 2026
 Grid ResilienceUS Energy Department Announces $237 Million Grid SCALED Funding ProgramExplore the DOE's $237 million Grid SCALED funding program and its goals to strengthen grid equipment supply chains, lower electricity costs, and improve resilience.By: Dr. Elena VoltOct 31, 2026
 UHV TransformersA Decade of UHV Power in Shandong: Province Leads in Station NumbersShandong UHV power leads China in station numbers. Explore a decade of grid development and its implications for electricity supply and business planning.By: Dr. Elena VoltOct 30, 2026
 Digital SeaChoosing a Composite Train Body Panel Manufacturer: Fire Safety and Quality ChecksChoosing a composite train body panels manufacturer? Learn how to verify fire test evidence, audit production quality, and avoid costly approval gaps before you buy.By: Captain Kenji SatoOct 29, 2026
 Subsea ROV/AUVOcean Infinity Deploys Six AUVs Together Beyond 5,000 MetresOcean Infinity reportedly deployed six HUGIN AUVs beyond 5,200 metres. Explore what concurrent deepwater missions could mean for seabed surveys and procurement.By: Captain Kenji SatoOct 29, 2026
 Grid ResilienceRenewable Energy Grid Balancing: How Storage and Demand Response Work TogetherExplore renewable energy grid balancing with storage and demand response. Learn how coordinated controls manage shortfalls, absorb surplus power, and improve grid reliability.By: Dr. Elena VoltOct 28, 2026