BDI: 1,842 ▼ 1.2%
COTTON NO.2: 84.12 ▲ 0.4%
LME COPPER: 8,432.50 ▲ 2.1%
FOOD SAFETY INDEX: 94.2 ARCHIVE_SECURED
OPTICAL INDEX: 11,204.09 STABLE
BDI: 1,842 ▼ 1.2%

SECTOR INDEX
V.24.08 ARCHIVE
Hot Articles
- Nonwoven Bonding Cost Data: Comparing Thermal and Chemical ProcessesExplore nonwoven bonding cost data to compare thermal and chemical processes, assess usable yield, and choose the best-value option for your application.
- Industrial Lasers to 2035: Automotive Lightweighting and Precision Welding Drive DemandExplore the industrial laser market outlook to 2035 and discover how automotive lightweighting and precision welding could shape demand and procurement.
- Choosing Geotextile Under Railway Ballast: Key Performance RequirementsChoosing geotextile under railway ballast? Explore essential filtration, drainage, strength and durability criteria to make a confident, project-specific selection.
Choosing a Composite Train Body Panel Manufacturer: Fire Safety and Quality Checks


A composite train body panel should not be approved on the strength of a fire certificate and an attractive unit price. The decisive question is whether the fire evidence covers the exact panel being purchased—and whether the manufacturer can reproduce that construction consistently throughout the order.
A lower quotation can become more expensive if qualification requires additional testing, finished panels need rework, or an undocumented material substitution invalidates the approval basis. Supplier selection therefore needs to connect three things: the project’s fire requirements, the tested panel configuration, and the controls governing serial production.
Define the panel’s duty before comparing quotations
“Train body panel” can describe an interior lining, an exterior cladding panel, or a load-bearing composite assembly. These products do not necessarily share the same fire requirements, mechanical duties, or acceptance criteria. Comparing quotations before establishing that distinction creates misleading price differences.
The enquiry should identify the installation location, drawing revision, attachment method, exposed surfaces, and whether the panel has a structural function. It should also specify relevant service conditions, including cleaning chemicals, moisture, temperature exposure, and exterior weathering where applicable.
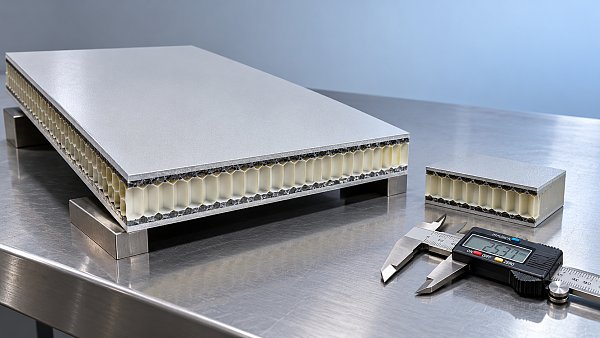
For a sandwich panel, the specification must describe more than its overall thickness. Skin reinforcement, resin system, core material, adhesive, surface finish, edge closure, and inserts all contribute to the delivered construction. Leaving these choices open allows suppliers to quote materially different products against the same description.
Separate mandatory acceptance requirements from preferences. Weight limits, dimensional tolerances, fire performance, and interface dimensions should have defined acceptance criteria. A preferred surface appearance should not carry the same contractual ambiguity as a mandatory safety requirement.
Establish which fire requirements actually apply
EN 45545-2 addresses requirements for the fire behaviour of materials and components used in railway vehicles. It is not a universal product approval, and a statement such as “EN 45545 compliant” does not establish suitability for every panel location.
Under the EN 45545 framework, the applicable hazard level—HL1, HL2, or HL3—is determined through the vehicle’s operating and design categories. The relevant requirement set depends on the component’s application. A large interior surface may fall under R1, but that designation should not be applied automatically to every interior or exterior composite panel.
The vehicle integrator’s approved fire specification should establish the required standard edition, requirement set, hazard level, and any project-specific provisions. Where the installation performs a fire-barrier function, reaction-to-fire evidence under EN 45545-2 alone does not demonstrate the required fire resistance.
For projects using another regulatory framework, evidence must be assessed against that framework. North American projects, for example, may reference NFPA 130 or applicable federal requirements, depending on the system and vehicle. A pass under one framework is not automatic equivalence under another.
Resolve these requirements before placing a production order. Asking a manufacturer to “meet railway fire standards” transfers ambiguity into the contract rather than removing it.
Read the test report against the proposed construction
The most useful fire document is the complete report, not a one-page certificate or a brochure displaying a standard number. The report should identify the laboratory, test methods, specimen description, results, and relevant preparation and mounting conditions.
Check laboratory competence for the actual methods involved. Accreditation to ISO/IEC 17025 is relevant, but its scope must cover the tests being relied upon. Accreditation is evidence of laboratory competence; it is not blanket certification of the supplier’s product range.
The central review is a line-by-line comparison between the tested specimen and the production bill of materials.
A fire report for a cured resin does not automatically qualify a finished sandwich panel. Likewise, evidence for an unfinished laminate should not be treated as approval for a painted, bonded assembly without a documented technical basis.
Not every variation necessarily requires a new test. Applicable rules may permit defined ranges, grouping, or extensions of results. Any such coverage should be documented and accepted through the project’s approval process—not inferred from a supplier’s statement that two materials are “equivalent.”
Check report authenticity, revision status, and sample identification. The supplier should explain how the tested sample relates to its material specifications and manufacturing records. An older report is not automatically unusable, but its relevance depends on the specified standard edition, unchanged construction, and project acceptance rules.

Audit the process that must reproduce the approved panel
A successful test establishes performance for the tested construction. It does not demonstrate that every subsequent panel will have the same resin content, cure state, bond quality, or finish thickness. These production variables are where quality assurance becomes directly relevant to fire compliance and service reliability.
ISO 9001 certification provides evidence of a quality management system within its stated scope. ISO 22163 adds railway-sector quality management requirements. Neither substitutes for product qualification, and certificates should be checked for the relevant manufacturing site and activities.
A supplier audit should follow one representative panel from incoming materials to final release. Request records that show what happens when a parameter falls outside its approved range, rather than relying only on written procedures.
- Incoming materials: batch identification, supplier documentation, shelf-life checks, and storage controls for resins, adhesives, prepregs, and cores.
- Manufacturing: controlled lay-up instructions, material quantities where relevant, vacuum or pressure records, cure cycles, and calibrated measuring equipment.
- Bonding: defined surface preparation, adhesive application, working-time limits, fixture conditions, and cure verification.
- Finishing: specified coating systems, preparation methods, and controls on applied thickness.
- Nonconformities: segregation, documented disposition, repair approval, and checks after repair.
The manufacturing route changes the emphasis of the audit. Infused panels require attention to resin flow and dry areas; prepreg processing requires control of storage, out-time, and cure; bonded sandwich assemblies need particular attention to bond-line integrity. A generic checklist cannot replace process-specific scrutiny.
Traceability should link the finished panel to relevant material batches, production records, inspection results, and approved deviations. If a material batch is later questioned, these records should allow the manufacturer to identify affected panels without placing the entire delivery population in doubt.
Make acceptance measurable before serial production
“Good surface quality” and “no defects” are poor acceptance terms. They leave both parties without an agreed basis for accepting or rejecting parts. Drawings and inspection plans should define critical dimensions, flatness, interface positions, edge condition, and allowable cosmetic imperfections.
First-article approval should confirm the production route, not merely the appearance of a hand-finished sample. The submitted panel should be accompanied by the agreed dimensional report, material traceability, process records, and evidence that inserts and attachments meet their specified duties.
Some defects require more than visual inspection. Internal voids, delamination, and disbonding may need non-destructive examination. However, prescribing ultrasonic inspection for every geometry without demonstrating its suitability can add cost without reliable detection. The method, reference standards, coverage, and acceptance limits must suit the laminate and core construction.
Mechanical verification should follow the panel’s function. Insert pull-out strength, attachment loads, stiffness, impact resistance, and fatigue can be relevant, but they should not be imposed indiscriminately. Fire compliance does not demonstrate structural adequacy, and a mechanically robust panel does not establish fire compliance.
For serial deliveries, define inspection frequency and release documentation. Identify which checks apply to every panel, which use sampling, and which are qualification tests. Safety-critical characteristics should not be treated as cosmetic sampling items.
Compare the cost of an accepted panel, not just a manufactured one
Quotations become comparable only when they include the same construction, evidence, inspection scope, and delivery conditions. A supplier excluding fire qualification, tooling validation, or inspection records has not necessarily offered a more efficient manufacturing solution; it may simply have quoted less work.
A useful comparison separates:
- Tooling, design-for-manufacture work, and first-article approval.
- Existing qualification evidence and any additional testing required.
- Recurring panel price, including finishing and inspection.
- Packaging, freight, import costs, and delivery terms.
- Repair, rejection, replacement, and warranty responsibilities.
Ask who pays if the proposed construction fails qualification and whether changes trigger new tooling or testing charges. Test ownership and access also matter: paying for qualification has limited value if the contract does not secure the reports and supporting information needed for project approval.
Production capacity should be assessed at the bottleneck operation. A stated monthly output is weak evidence unless supported by available moulds, cure equipment, finishing capacity, inspection resources, and existing commitments. Extra moulds will not resolve a constrained bonding or painting operation.
Packaging deserves explicit acceptance criteria. Large panels can leave the factory within tolerance and arrive with distorted edges, damaged finishes, or stressed inserts. Transport supports, stacking restrictions, moisture protection, and handling points should match the panel design.
Keep the approval basis intact after contract award
The purchasing specification should freeze the approved bill of materials, drawings, manufacturing route, and applicable qualification evidence. Changes to resin, core, adhesive, finish, manufacturing site, or critical processing conditions should require notification and approval before implementation.
“Equivalent material” is not an adequate unilateral substitution clause. A replacement may meet a mechanical datasheet while falling outside the fire evidence. The change process must assess both product performance and the continued validity of the approval basis.
A composite train body panels manufacturer is a credible choice when it can show a continuous evidence chain: project requirement, representative test construction, controlled production, and documented release. An unexplained break in that chain is grounds to withhold approval, regardless of unit price.
Where gaps are limited and resolvable, a conditional award can tie production release to specific evidence and acceptance milestones. Where the tested construction cannot be identified, substitutions are uncontrolled, or traceability cannot isolate affected parts, a lower price is not a defensible trade-off.
Recommended for You
 Technical FabricsNonwoven Bonding Cost Data: Comparing Thermal and Chemical ProcessesExplore nonwoven bonding cost data to compare thermal and chemical processes, assess usable yield, and choose the best-value option for your application.By: Chloe DuboisNov 08, 2026
 Fiber LasersIndustrial Lasers to 2035: Automotive Lightweighting and Precision Welding Drive DemandExplore the industrial laser market outlook to 2035 and discover how automotive lightweighting and precision welding could shape demand and procurement.By: Dr. Hideo TanakaNov 07, 2026
 Technical FabricsChoosing Geotextile Under Railway Ballast: Key Performance RequirementsChoosing geotextile under railway ballast? Explore essential filtration, drainage, strength and durability criteria to make a confident, project-specific selection.By: Chloe DuboisNov 07, 2026
 Digital SeaChoosing Rail Welding Equipment for Maintenance: Field Conditions and Weld TypesChoose rail welding equipment for maintenance with confidence. Compare welding methods, field constraints, inspection needs, and lifecycle costs.By: Captain Kenji SatoNov 06, 2026
 Digital SeaIndia Broadband Forum Urges Stronger Submarine Cable ResilienceIndia’s submarine cable resilience is in focus as the Broadband India Forum urges faster repairs, more vessels and stronger landing infrastructure.By: Captain Kenji SatoNov 06, 2026
 Digital SeaChoosing a Railway Network Switch Supplier: Reliability and Support CriteriaChoosing a railway network switch supplier? Compare reliability, standards evidence, cybersecurity, and lifecycle support to reduce project risk.By: Captain Kenji SatoNov 05, 2026
 Grid ResilienceUS Grid Equipment Import Ban Raises Cost and Implementation ConcernsThe US grid equipment import ban raises concerns over costs and delivery delays. Explore how unclear criteria could affect procurement and supply chains.By: Dr. Elena VoltNov 05, 2026
 Digital SeaRailway Coupler Price: How Type and Specifications Affect QuotesRailway coupler price depends on type, specifications, and order scope. Learn how to compare quotes, avoid hidden costs, and make a confident buying decision.By: Captain Kenji SatoNov 04, 2026
 Grid ResilienceGlobal Smart Grid Companies Raise $3 Billion in First Nine Months of 2026Global smart grid companies raised $3 billion in the first nine months of 2026. Explore the funding breakdown and potential implications for buyers and suppliers.By: Dr. Elena VoltNov 04, 2026
 Digital SeaChoosing Wholesale Pet Toys: How to Evaluate Suppliers and Minimum OrdersWholesale pet toys: learn how to assess suppliers, compare minimum orders and landed costs, and reduce inventory risk before you buy.By: Captain Kenji SatoNov 03, 2026
 Digital SeaSustainable Packaging Design: How to Choose Materials and Reduce WasteDiscover how sustainable packaging design helps reduce waste, protect products, and control costs with practical material choices and proven testing strategies.By: Captain Kenji SatoNov 02, 2026
 Technical FabricsUSMCA's First Joint Review Puts Textile Supply Chain Rules in FocusUSMCA's first joint review puts textile supply chain rules in focus. Explore potential impacts on origin compliance, sourcing and tariff treatment.By: Chloe DuboisNov 02, 2026
 Digital SeaManufacturing KPI Benchmarking: How to Compare Production PerformanceBenchmarking KPI manufacturing performance? Learn how to compare OEE, quality and downtime, identify meaningful gaps, and turn insights into practical improvements.By: Captain Kenji SatoNov 01, 2026
 Smart MetersCCI Approves Adani Energy Solutions' ₹305 Billion Acquisition of IntelliSmartCCI approves Adani Energy Solutions' ₹305 billion acquisition of IntelliSmart. Discover what the deal could mean for India's smart meter market.By: Dr. Elena VoltNov 01, 2026
 Digital SeaChoosing a Coin Laundry Machinery OEM: What Buyers Should EvaluateChoosing a coin laundry machinery OEM? Compare machine specifications, payment integration, lifecycle costs, and support to make a confident buying decision.By: Captain Kenji SatoOct 31, 2026
 Grid ResilienceUS Energy Department Announces $237 Million Grid SCALED Funding ProgramExplore the DOE's $237 million Grid SCALED funding program and its goals to strengthen grid equipment supply chains, lower electricity costs, and improve resilience.By: Dr. Elena VoltOct 31, 2026
 UHV TransformersA Decade of UHV Power in Shandong: Province Leads in Station NumbersShandong UHV power leads China in station numbers. Explore a decade of grid development and its implications for electricity supply and business planning.By: Dr. Elena VoltOct 30, 2026
 Digital SeaChoosing a Composite Train Body Panel Manufacturer: Fire Safety and Quality ChecksChoosing a composite train body panels manufacturer? Learn how to verify fire test evidence, audit production quality, and avoid costly approval gaps before you buy.By: Captain Kenji SatoOct 29, 2026
 Subsea ROV/AUVOcean Infinity Deploys Six AUVs Together Beyond 5,000 MetresOcean Infinity reportedly deployed six HUGIN AUVs beyond 5,200 metres. Explore what concurrent deepwater missions could mean for seabed surveys and procurement.By: Captain Kenji SatoOct 29, 2026
 Grid ResilienceRenewable Energy Grid Balancing: How Storage and Demand Response Work TogetherExplore renewable energy grid balancing with storage and demand response. Learn how coordinated controls manage shortfalls, absorb surplus power, and improve grid reliability.By: Dr. Elena VoltOct 28, 2026
 Subsea ROV/AUVSeaber Introduces 13 kg RAVEN AUV to Target Mine Countermeasure CostsSeaber’s 13 kg RAVEN AUV targets lower mine countermeasure costs with two mission configurations. Explore its potential value for naval operations and procurement.By: Captain Kenji SatoOct 28, 2026
 Digital SeaBallast Water Management Rules: IMO vs. USCG Compliance RequirementsBallast water management rules explained: compare IMO and USCG approvals, operating limits, and records. Get practical checks to reduce compliance risks and costly port delays.By: Captain Kenji SatoOct 27, 2026
 Subsea ROV/AUVEni Signs Main Cronos Contracts, Moving Gas Project into ExecutionEni’s Cronos gas project enters execution as major contracts are signed. Explore the Cyprus development, Egypt processing plans and key milestones toward first gas in 2028.By: Captain Kenji SatoOct 27, 2026
 Aseptic FillingWhich Tests Verify Commercial Sterility in Aseptically Filled Foods?Explore aseptic filled food tests, from incubation and microbiology to package integrity. Learn how connected evidence supports confident commercial sterility release decisions.By: Marcus SterlingOct 26, 2026
 Fabric LogicWater-Free Textile Printing: Fabric Compatibility and Pretreatment LimitsExplore water free textile printing for polyester, cotton, and blends. Learn pretreatment limits and key durability tests to choose the right process and avoid costly production mistakes.By: Chloe DuboisOct 26, 2026
 Dyeing MachinesHow Waterless CO2 Dyeing Works—and Why Polyester Is a Strong FitDiscover how waterless dyeing with supercritical CO2 colors polyester, why this fiber is a strong fit, and what to verify for consistent shades and measurable resource savings.By: Chloe DuboisOct 26, 2026
 Smart MetersSourcing Smart Meter Structural Components from China: An RFQ ChecklistExport smart meter structural components from China with confidence. Use this RFQ checklist to compare materials, tooling, quality, and delivered costs—and avoid costly sourcing mistakes.By: Dr. Elena VoltOct 26, 2026
 Optical SensorsEvaluating an Optical Detection Factory: Calibration and RepeatabilityEvaluate an optical detection factory with confidence. Learn how calibration, traceability, and repeatability trials reveal production reliability and help you choose the right supplier.By: Dr. Hideo TanakaOct 26, 2026
 Precision LensesChoosing a Welding Optics Supplier in China: Coatings and Damage ThresholdsCompare welding optics supplier China options for coating quality, verified damage thresholds, and batch consistency. Learn how to reduce downtime and buy with confidence.By: Dr. Hideo TanakaOct 26, 2026
 Aseptic FillingStainless Steel Mixing Tanks: Cleaning Access Checks Before PurchaseBuying stainless steel mixing tanks? Check cleaning access, CIP coverage, drainage, and acceptance tests before purchase to reduce changeover headaches and make a confident choice.By: Marcus SterlingOct 26, 2026
 Digital SeaRail Communication Bandwidth in Europe: GSM-R and FRMCS Bands ExplainedRail communication bandwidth Europe: explore GSM-R and FRMCS bands, compare 900 MHz and 1900 MHz spectrum, and discover key checks for smarter network planning.By: Captain Kenji SatoOct 26, 2026